

 30 / 50

A D V A N C E D M A T E R I A L S & P R O C E S S E S | A P R I L 2 0 1 7
3 0
I
f it wasn’t for metal welds, our world
would literally fall apart. Yet most
people are largely unaware of the in-
calculable load and responsibility that
welds bear for our safety, satisfaction,
and well-being. Nor are they likely to
appreciate the high cost of weld failures
and the relentless pursuit to improve the
tools and techniques available to indus-
try to measure the strength and longev-
ity of metal welds.
Advanced Materials &
Processes
spoke with Keith Thompson,
product manager of microanalysis for
Thermo Fisher Scientific, who not only
understands the need for better tools and
methods, but is workingwith others to do
something about it.
AM&P: Can you discuss the
importance of measuring
metal welds and the
implications for industry?
KT:
Welds canbe theweakest point
in fabricated metal structures. And the
welding process itself can degrade the
properties of metals and alloys due to
microstructural changes caused by the
heating and cooling cycle. It is quite
common for manufacturers to conduct
hundreds of tests on weld develop-
ment, using optical microscopes, for
example, to check welds for cracking,
porosity, and general integrity. In addi-
tion, air testers and dyed water tests are
used to probe for leaks, while mechan-
ical pull tests are used to measure weld
strength. But if the tests detect only
symptoms and not the cause, which is
often the case, welds that pass inspec-
tion at the factory may still fail earlier
than expected in the field.
AM&P: What are some of the
challenges manufacturers
face in their weld testing
processes?
KT:
Many manufacturers conduct
lifetime tests by running products until
failure. Automakers, for example, will
drive test vehicles in different environ-
ments and under a variety of conditions
until a part fails. Then they take the part
and spend months trying to improve it
before running additional tests, then
repeat the process. This kind of symp-
tomatically driven “make it and break
it” development process can take two
to five years to wring out a design—an
unacceptably long time, especially
in the highly competitive automotive
market.
In order to minimize tradeoffs
between time-to-market and product
reliability, safety, and service life, in-
dustry as a whole is investing heavily
in developing analytical instrumenta-
tion technology and test procedures
that more directly and reliably expose
root causes of failures. These efforts are
paying off. In the case of metal welds,
manufacturers now have access to
powerful imaging techniques such as
electron backscatter diffraction (EBSD),
meaning they no longer have to wait
for parts to fall off test vehicles or de-
velop discernible cracks to begin fixing
them. Instead, they just need to put a
weld sample under a scanning electron
microscope and look for telltale micro-
structural changes.
AM&P: Could you give us an
example of a microstructural
change caused by welding?
KT:
Grains in metals tend to be
nonpreferential in shape and direction,
which is why metals are isotropic by na-
ture, exhibiting properties that are the
same in any direction. Now if I join two
pieces of metal with a weld bead that
goes from left to right, the grains along
the weld are likely to become larger,
possibly more elliptical in shape, and
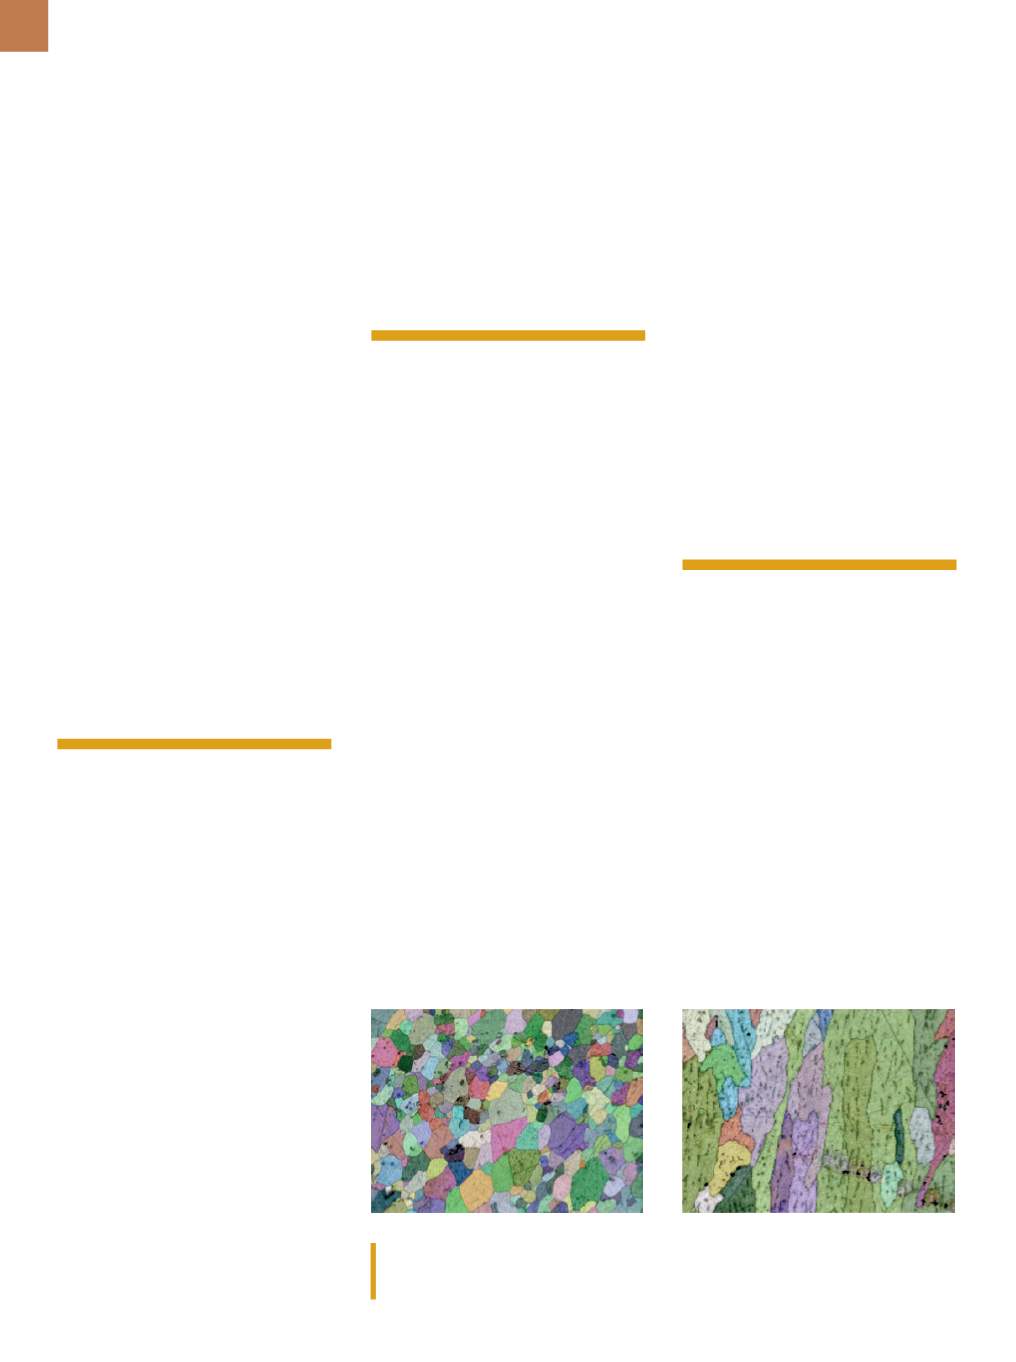
aligned to the right (Fig. 1a and 1b). The
resulting structure might be stronger in
the direction of the weld, but weaker
laterally. I can confirm this using EBSD
on a weld sample by applying a force in
TECHNICAL SPOTLIGHT
PUTTINGWELDS TO THE TEST
Advanced instrumentation combined with e ective
test procedures gives manufacturers an edge in
measuring and analyzing welds.
Fig. 1 –
EBSD Euler maps reveal microstructural changes in aluminum caused by welding.
Note the di erences in grain size and orientation between (a) the bulk material and (b) that in
the weld region.
(a)
(b)