

 37 / 62

iTSSe
TSS
A D V A N C E D
M A T E R I A L S
&
P R O C E S S E S | F E B R U A R Y
2 0 1 6
3 7
iTSSe
TSS
7
FEATURE ARTICLE
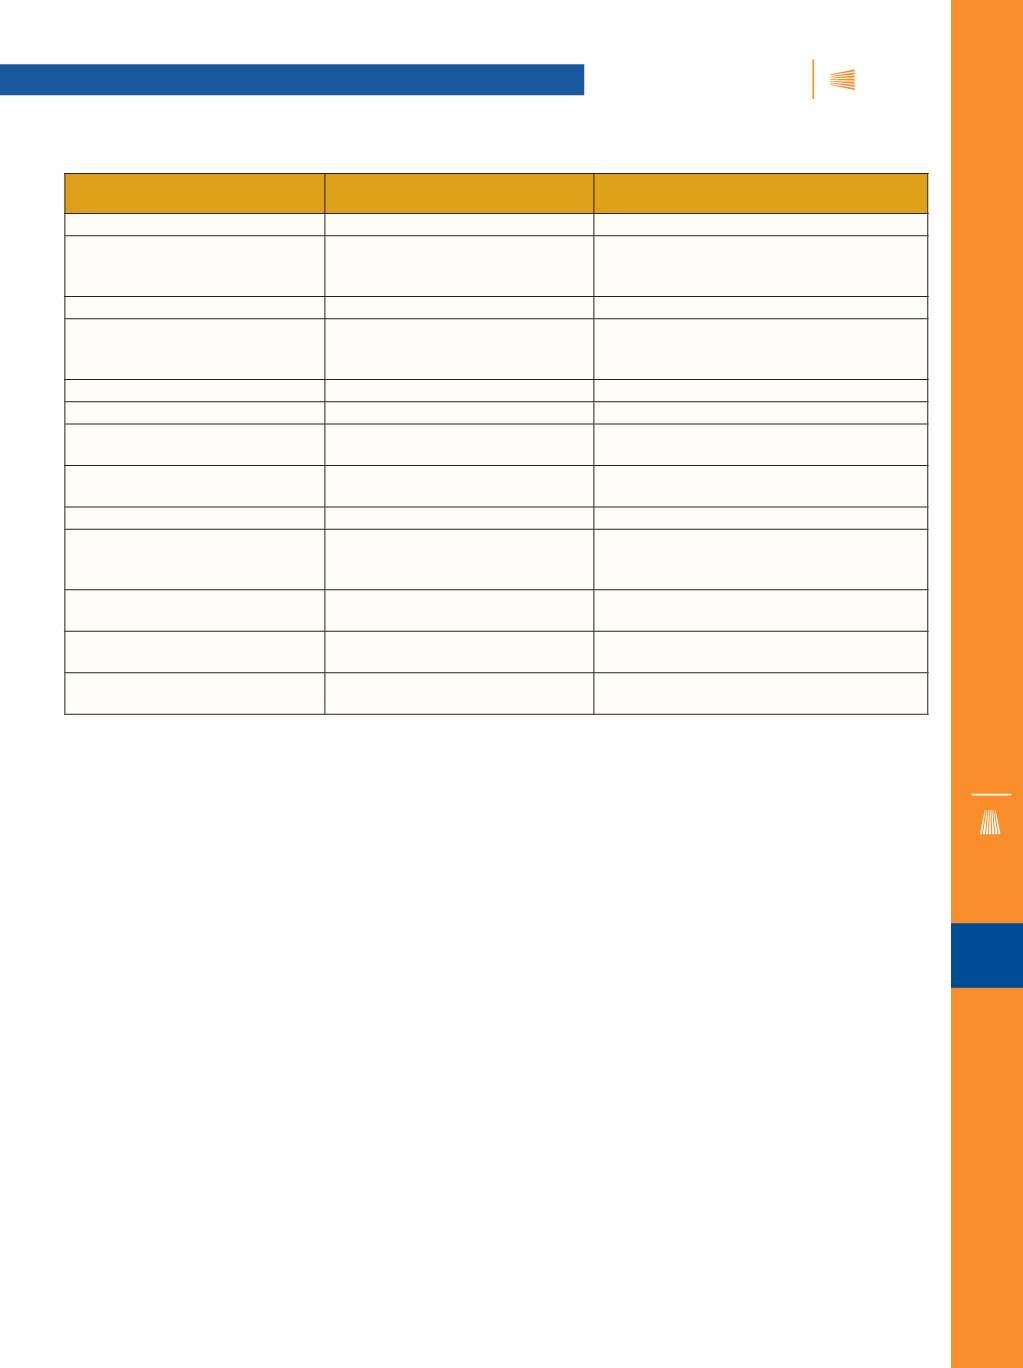
TABLE 2—TSAC VERSUS CONVENTIONAL ORGANIC COATINGS
Features
Organic coating system
TSA + sealer coat
Surface preparation
25-50 micron (S a 2
1/ 2
)
>65 micron (S a 3)
Process temperature
Ambient
Torch at >1000
0
C
Metallizing at >675
0
C
Substrate at 120-150
0
C
Productivity
200 m
2
per shift
20-25 m
2
/shift
Accessibility
Using brush can cover entire area
Coating of nooks and corners, T-welds,
assembled components, and recess
areas is nearly impossible.
Welding/repair/rework
Possible
Questionable
Hot permit
Not required
Required (even at later stage)
Safety
Minimum protection
Complete protection (metal fumes, UV,
thermal radiation and noise hazard)
Contractors
Quality contractors are easily
available
Limited vendor base with proven capability
Handling of coated components
Not an issue
Same quality cannot be restored
Corrosion protection in splash zone
Other proven coating systems
are available. 1500 microns
DFT are specified.
Adequate TSA coating (200 microns)
for splash zone
Operator shift time
One operator can work continuously
Need to relieve operator after
maximum of two hours
Top coat application
Primers are available where coating
interval can vary up to six months
Immediate sealer coating (within six hours)
Rework on splash zone
Systems are available
Difficult to achieve surface finish and coating
application in low tide duration
low lifecycle costs. These benefits outweigh the drawbacks,
which include the necessity of using a hot process, sensitiv-
ity to dust, wind, and moisture, potential for operator error,
and shock and noise hazards.
The procedural details, readiness report, and inspec-
tion checklist were prepared to ensure guaranteed quality
in every aspect of this project. Thermal spray aluminum re-
quires rigorous process control over the entire operational
sequence, from initial blasting to spraying the final sealer
coat. Specifications provided by the client, PMC, were quite
stringent, with required parameters that are only achiev-
able at laboratory scale. Interactions with PMC engineers
regarding various technical issues served to make the pro-
cess conditions less stringent while adhering to internation-
ally accepted parameters. Issues such as adhesion bond
strength, procedure qualification record, surface prepara-
tion, dew point, and final shade of sealer coat on the jacket
splash zone were all successfully resolved.
Table 2 summarizes limitations of TSAC with respect to
widely adopted organic coatings for the splash zone. When
the coating application is to be done “in yard,” constraints
are imposed such as absence of control over environmental
conditions. Further, because in-yard application occurs in an
open environment, safety is a top concern and the areamust
be barricaded. Operators and personnel in the vicinity must
use ear protection and protective UV glasses. The process is
labor intensive and proper ventilation must be in place for
operator health. Further, aluminum metal dust is prone to
cause electric shocks and must be appropriately contained.
Once the coating process is underway, coated objects must
be handled with care using canvas slings and shrink wrap.
Proper masking to protect surfaces not to be coated is an-
other vital step that must occur before TSAC application.
Paying close attention to all of these parameters will enable
successful achievement of bond strength for a long and
maintenance-free service life with an optimized lifecycle
cost.
PROPER APPLICATION OF TSAC
OVERCOMES CONSTRAINTS
•
Repair/touch-up/patchwork are very difficult once TSA
application is complete, compared to conventional
paint. Therefore, the structure was released for TSA
coating only after all QA/QC reports were received and
cleared. All QA/QC requirements of such structures were
completed on time with the help of the QC team to avoid
any downtime. The slings of the assembly cranes were
wrapped with cloth and care was taken to avoid any
repairs.