

 39 / 62

ADVANCED MATERIALS & PROCESSES •
AUGUST 2014
39
i
T
S
S
e
7
Safety in Thermal Spray
Settings: Part 1
Much of the following material was developed
by members of ASM International’s Thermal Spray
Society Safety Committee.
W
orkplace safety is not a subject that typically capti-
vates an audience, but in the thermal spray trade,
hazards of all types are faced on a daily basis. Safety talk
is typically thought of as a matter of common sense, and
formal programs to communicate and enforce safe prac-
tices can seem unnecessary or, in worst case scenarios, as
an opportunity to issue penalties based on grudges, rather
than evenhanded enforcement. Unlike truly dangerous
workplaces, such as shipyards or construction sites, where
situational awareness is necessary to stay alive and well,
the extra cost and time safety programs consume can make
them unattractive in comparatively comfortable thermal
spray shops. However, compelling reasons to embrace the
safety topic still exist.
For starters, maintaining a safe workplace is the law.
Title 29 Part 1900 of the Code of Federal Regulations out-
lines the mandate, reach, and policies of the Occupational
Safety and HealthAdministration (OSHA). Despite rumors
that OSHA’s jurisdiction does not apply to shops below a
certain size, there is not likely a thermal spray or welding
shop immune to OSHA’s regulations.
Because of this, safety discussions can broaden aware-
ness of operating requirements that some smaller facilities
might not know. It is also important for frontline employ-
ees to be aware of the potential hazards faced daily in order
to motivate them to voluntarily take appropriate precau-
tions. The topic can be discussed clearly and concisely in
this manner, making it easier to ensure requirements are
met. Involving people at every operational level during the
development of plant policies ensures that employee safety
will not hinder workload.
Dust and fume hazards
Another reason safety discussions are especially im-
portant in the thermal spray workplace is that hazards ap-
pear throughout the coating operation, from incoming
orders to final inspection. Dust and fume hazards are an
excellent example. Technically speaking, dust consists of
airborne fine solid particles such as fractured grit blasting
media or thermal spray powders, which can irritate lungs
and mucous membranes. Fumes are finer suspended
particles released when materials are heated or burned, for
example, when thermal spray feedstock enters the combus-
tion zone or plasma plume of a spray gun.
Dust and fume exposure occurs during degreasing,
blasting, powder handling, spraying, sealing, and even
maintenance and cleaning. Some thermal spray fumes,
such as hexavalent chromium, are known cancer causing
agents. Vapors are emitted by liquids that evaporate at
room temperature, including solvents such as acetone
and trichloroethane, which are commonly used for
cleaning and degreasing parts. Inhaling these vapors can
damage the lungs and internal organs.
Most dusts and fumes common in spray shops irritate
the lungs, but others have more reactive effects. For exam-
ple, nickel, cobalt, and chromium can cause eczema and
contact dermatitis. Fumes released during twin arc wire
spraying of zinc can cause nausea, fever, and other flu-like
symptoms, known as “zinc fever.” The hazard of the air-
borne carcinogen hexavalent chromium is so acute that the
code places specific requirements on employers who are
known generators. Part 1910.1026 requires regular physi-
cal testing of employees who may be exposed, and makes
the provision and handling of specialized protective cloth-
ing, among other things, the employer’s responsibility.
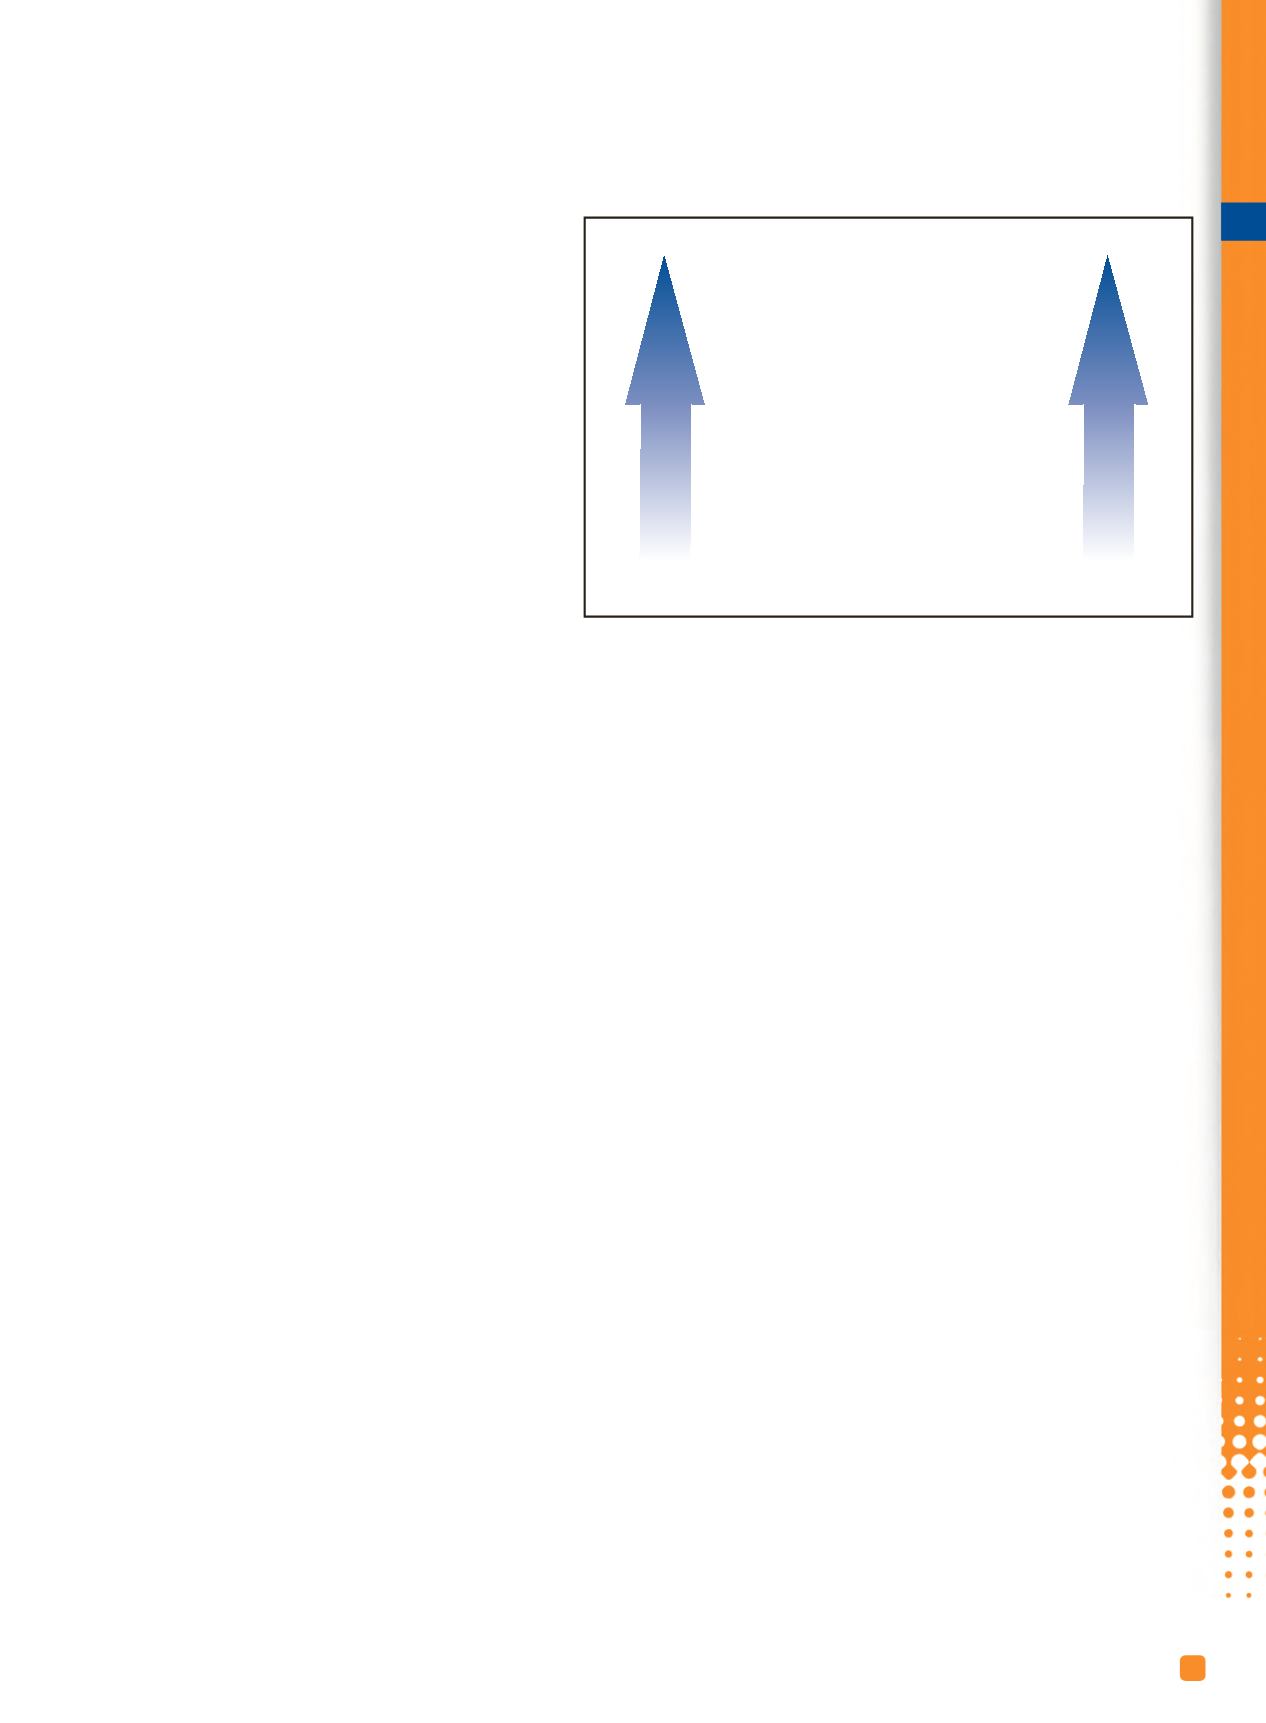
As with all hazard categories, several methods to elimi-
nate or remediate hazards caused by dust and fumes exist
(Fig. 1). The most effective option is to eliminate the hazard
altogether, though this is seldom an option. The next best al-
ternative is to substitute a less hazardous material or process.
Depending on the application, this also may not be a viable
alternative. Engineering controls are methods by which
equipment can be added or a process design can be modified
to reduce or eliminate the hazard to employees. In the case
of dust and fumes, use of sufficient air filtration is an engi-
neering control that can ensure contaminated air is drawn
away from operators, removing the hazard. It also effectively
cleans the air before it is reintroduced to the environment.
Administrative controls are the next layer of hazard
mitigation available to employers. These consist of poli-
cies and procedures that mandate specific safe working
practices for each workplace hazard. Training, signage,
procedures, and employee exposure are all administrative
controls that can aid in the mitigation of dust and fume haz-
ards. Finally, personal protective equipment (PPE), such
as dust masks and gloves, protect employees from harm
when direct contact with a hazard is likely. Though it is
perhaps the most common workplace safety measure, PPE
is considered the least effective measure because it depends
on employee participation and supervision.
iTSSe
Fig. 1 —
Hierarchy of controls. Courtesy of www.cdc.gov/niosh/docs/2013-136.
Look for
Part 2 of
this article
in the
November/
December
issue of
iTSSe.
Elimination
Design hazard out
Substitutions
Use alternative materials or processes
Engineering controls
Isolation and guarding
Administrative controls
Training and work scheduling
Personal protective equipment
Last resort
Best
Control
effectiveness
Best
Business
value