

 38 / 62

ADVANCED MATERIALS & PROCESSES •
AUGUST 2014
38
i
T
S
S
e
6
bores, which is achieved
by either using cast iron
liners or electroplating
with nickel and silicon
carbide.
PTWA was codevel-
oped by Ford Motor Co.,
Dearborn, Mich., and Flame-Spray
Industries Inc., Port Washington,
N.Y.,
[1-7]
in an effort to eliminate the
need for cast iron liners and further reduce weight. In this
process, a high temperature (>10,000°C) plasma jet is cre-
ated between a nonconsumable electrode and a consumable
composite ferrous wire with a 1.6 mm diameter (Fig. 1).
The plasma melts and atomizes the ferrous wire, which is
continuously fed into a rotating spray gun that fits within
the cylinders (Fig. 2). Pressurized air atomizes and acceler-
ates metal droplets (20 to 30 µm diameter) onto the internal
surface of engine block cylinders. The molten composite
wire oxidizes and builds up a rapidly solidified ferrous
structure consisting of nanocrystalline iron and ferrous-
oxide to a final thickness of about 150 µm.
The resulting surface structure of the composite coating
promotes favorable lubrication, low friction, wear resistance,
improved heat transfer, and decreased bore distortion. Ford
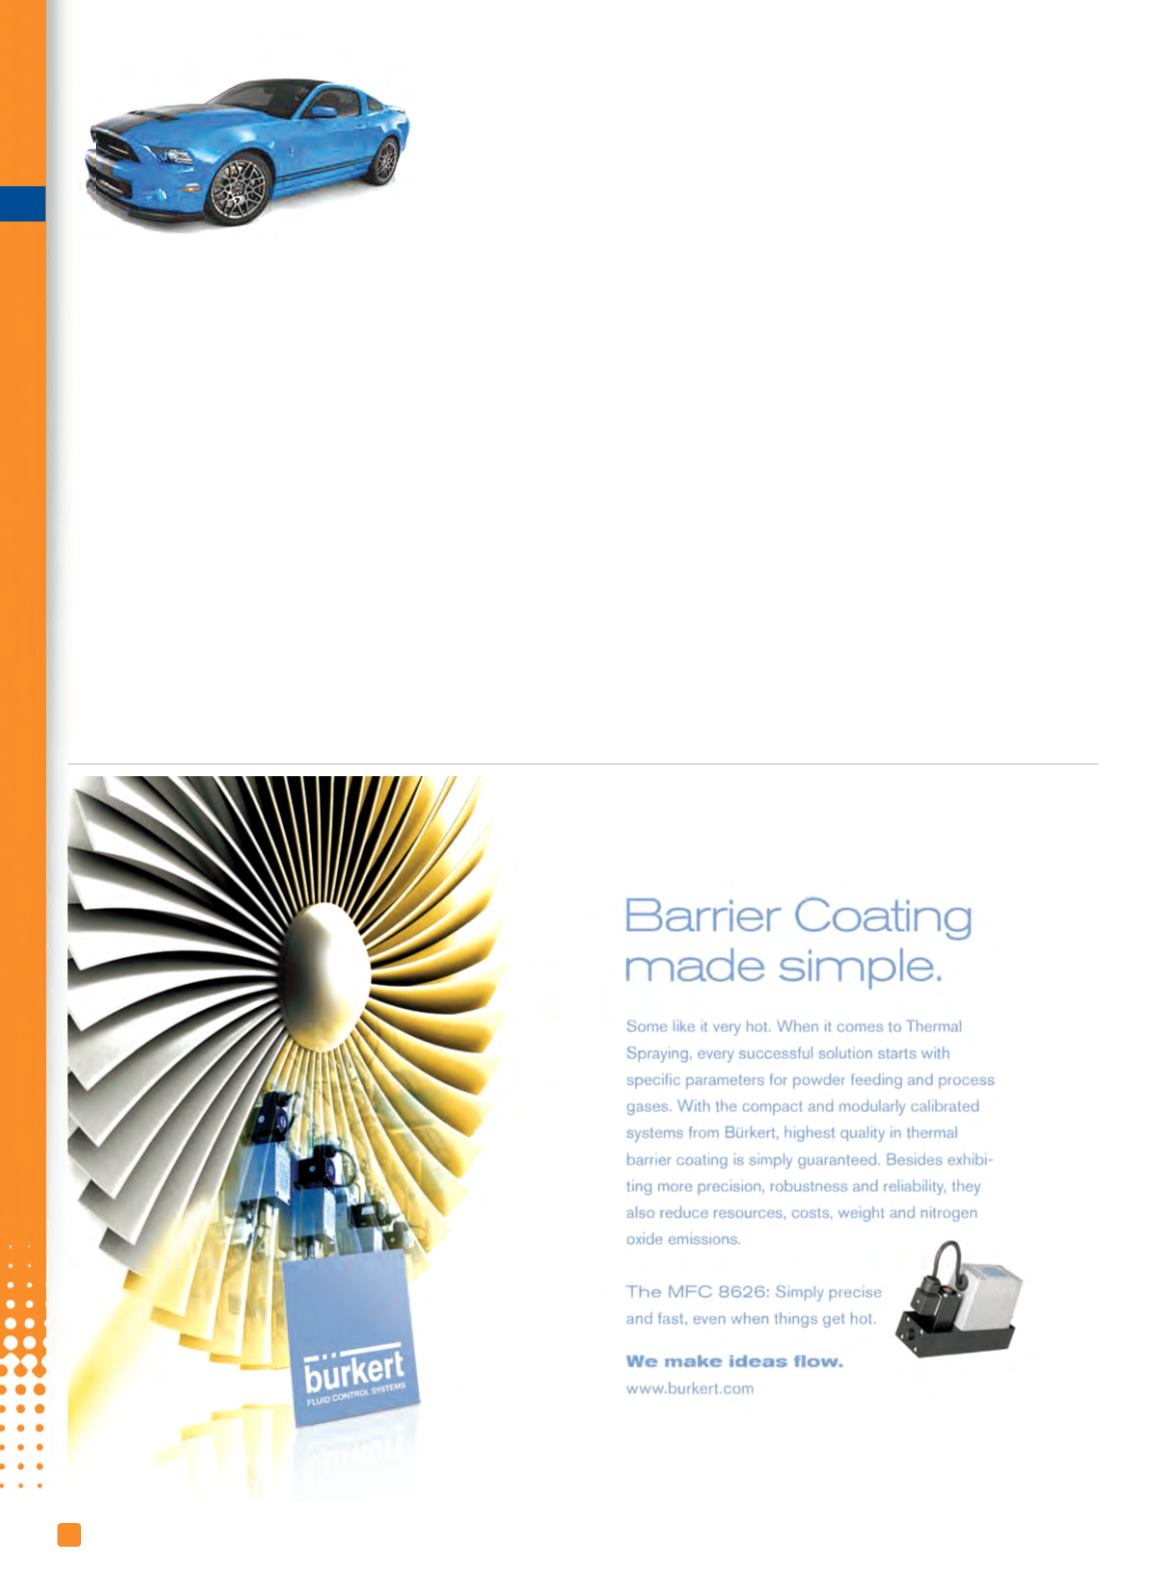
implemented the technology in their 2011 GT500 Shelby
Mustang 5.4-L V8 (Fig. 3)
[8]
. The PTWA process eliminated
approximately 3.8 kg of cylinder liners compared with pre-
vious models
[8]
.
iTSSe
F
or more information:
Julio Villafuerte, Ph.D., P.Eng, is cor-
porate technology strategist at CenterLine Windsor Ltd., 595
Morton Dr., Windsor, Ontario, Canada, 519.734.8868 ext. 474,
julio.villafuerte@cntrline.com,
cntrline.com/en.References
1. D. Marantz, et al., U.S. Patent 5,808,270, High Deposition
Rate Thermal Spray using Plasma Transferred Wire Arc, 1998.
2. J.Baughman, et al., U.S. Patent 5,938,944, Plasma Transferred
Wire Arc Thermal Spray Apparatus and Method, 1999.
3. D. Marantz, et al., U.S. Patent 6,372,298, High Deposition
Rate Thermal Spray using Plasma Transferred Wire Arc, 2002.
4. J. Chancey, et al., U.S. Patent 6,559,407, Cathode Assembly
for an Electric Arc Spray Apparatus, 2003.
5. K. Bobzin, et al., Thermal Spraying of Cylinder Bores with
the PTWA Internal Coating System, Conf. Proc., ASME Inter-
nal Combustion Engine, Charleston, SC, ICEF07-1745,Oct.
14-17, 2007.
6. K. Bobzin, et al., Coating Bores of Light Metal Engine Blocks
with a Nano Composite Material using PTWAProcess,
J. Therm.
Spray Techn.,
17 (3), p 344-351, 2008.
7. C. Verpoort and T. Schlaefer, Thermal Spraying of Nano-
Crystalline Coatings for Al-Cylinder Bores, SAE Technical
Paper, 2008.
8. Ford Motor press release,
http://media.ford.com/im- ages/10031/2011_GT500_Engine.pdf,Feb. 2010.
9. Comau, commercial system,
www.comau.com/eng/offering_ competence/powertrain/manufacturing/Pages/smart_spray.aspx,2014.
Fig. 3 —
Ford Mustang
Shelby GT500.